
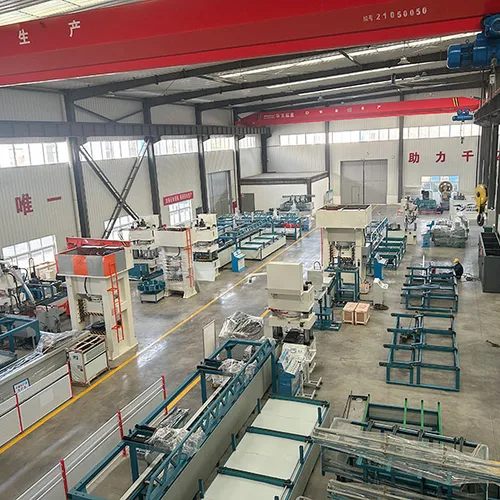
Mining Anchor Plate (Roof Bolt Plate) Automatic Production Line
最小起订量: 1套
- Altitude:
- < 1000 m
- Ambient operating temperature:
- –15°C to +40°C
- 参考价格:
- USD $100000.00 - $600000.00
- 最小起订量:
- 1套
- 交货期:
- 60天
- 供货能力:
- 1套/周
- 装运港:
- qingdao/Khorgos

产品特点与应用
The production line enables a fully automated workflow from raw material feeding → coordinated hydraulic press stamping and forming → finished product output and palletizing, with multiple design solutions available for customer selection. It can use coiled plates or strip steel as raw materials, with servo feeding. The product's dimensional tolerances can be adjusted according to actual requirements. Multiple pre-feeding design options ensure production efficiency. Dies are custom-made according to drawings or samples, and are designed for integrated output — combining shearing, punching, and forming in one step. An automatic palletizer (magnetic feeder, three-axis联动 palletizer) is available as an option, significantly reducing labor intensity and ensuring safe production. Processable Specifications: 120 to 300 mm anchor plates (customizable)
Mining Anchor Plate (Roof Bolt Plate) Automatic Production Line
I. Overall Process Flow
-
Tray models produced: 150-10 and 300-16 disc trays.
-
An overhead crane places stacked sheets onto the feeding rack → Chain conveyor transfers them to the waiting production area → Gantry-type pneumatic lifting magnetic suction servo feeder loads sheets onto the preparation feeder → Steel sheets are conveyed → Servo manipulator feeder (driven by a servo motor, capable of precisely adjusting feed size and speed) → Hydraulic forming → Output → Chain conveyor → Double stacker/palletizer.
-
-
Other trays or guard plates: Produced after mold change.
II. Equipment Operating Environmental Conditions
-
Installation location: Indoor site
-
Altitude: < 1000 m
-
Ambient operating temperature: –15°C to +40°C
III. Main Technical Parameters
-
Power supply: 380 V working voltage
-
Raw material length: 3 m – 6 m (customizable)
-
Equipment dimensions: approx. 15 m (L) × 5 m (W) (adjustable)
-
Power: approx. 48 kW (feeding system ~18 kW, hydraulic press 30 kW)
-
Equipment efficiency:
-
150×10 trays: ≥ 3000 pieces per 8 hours
-
300×16 trays: ≥ 800 pieces per 8 hours
-
-
Operators required: 2 per set – 1 for equipment operation and loading, 1 for bundling.
IV. Main Components
The tray production line mainly consists of: electric storage rack, pneumatic magnetic suction feeder, preparation feeder, magnetic feeding device, press, molds, output roller device, finished product conveyor, automatic stacker/palletizer, electrical control cabinet, etc.
(1) Electric Storage Rack
An overhead crane places stacked sheets onto the storage rack. By pressing buttons, the motor drives the reducer and conveys the sheets via chain to the waiting production area.
Advantages: Sheets can be loaded by the overhead crane during production; multiple stacks can be placed side by side in the waiting area, and automatic sequential feeding can be achieved by changing parameters on the display screen. This reduces loading time and lowers operator workload.
(2) Pneumatic Lifting Magnetic Suction Loading Device
Composed of cylinders, return auxiliary devices, servo motor travel system, electromagnets, etc. It can lift steel plates up to 900 kg to the preparation conveyor.
Advantage: Allows pre-feeding during production.
(3) Preparation Feeder
A motor drives the conveyor to transport sheets to the production area. Both sides of the conveyor rollers are equipped with automatic straightening and correcting devices for raw material. After correction, sheets are fed to the coordinate zero point (adjustable via the control cabinet text panel) to prepare material for the magnetic feeding device.
Advantage: Can feed material to the zero point in advance while the previous sheet is still being processed, enabling continuous production without stopping.
(4) Magnetic Feeding Device
Composed of a servo motor, electromagnets, slide rails, etc. When the raw material is sent to the coordinate zero point by the preparation feeder, the magnetic feeding device automatically starts. First, it clamps the raw material; the electromagnets are energized to pick up the sheet, and the feeding arm is driven by the servo motor via rack and pinion to the fixed point of the press. The electromagnets are de-energized, and the feeding arm returns to the zero point to press down and pick up the next sheet, while the press produces finished parts. When the remaining sheet on the feeding arm reaches a certain size (adjustable via PLC), the loading device automatically starts to prepare the next sheet. This cycle repeats, saving waiting time and improving efficiency. It enables automatic feeding of the tail end material without the need for side cylinders.
Advantage: Solves the problem of producing the last piece; the output roller chain directly discharges the finished products, with no side cylinders, saving cycle time.
(5) Molds
Integrated shear, punching, and forming direct‑output type molds are supplied according to customer requirements.
(6) Press
A 500‑ton three‑beam four‑column hydraulic press or an arm‑type press is available per customer request.
(7) Output Roller Device
Allows finished trays to slide freely. It is detachable, with a 1‑meter clearance for easy mold change.
(8) Finished Product Conveyor
Motor‑driven, it transports finished trays to the automatic stacker/palletizer.
(9) Automatic Stacker/Palletizer (Three‑Axis Linkage Stacker / Magnetic Suction Stacker)
-
Magnetic suction stacker: Suitable for 150×150×10 trays. The stacking platform is driven by a servo motor through a reducer to rotate a turntable. The turntable size is customizable, with annular stations on top. By changing parameters in the servo driver, the magnetic suction arm and the servo turntable are perfectly synchronized, allowing trays to be neatly arranged in sequence on each station. It has 12 stations, with 5/10 pieces per stack (adjustable). Stacking efficiency: approx. 6.5 seconds per tray.
-
Three‑axis linkage stacker: Suitable for 300×16 trays. The equipment is designed with three‑axis linkage, using two servo motors to control movement in the Y and Z axes respectively, while X‑axis movement is controlled by a cylinder. It offers high positioning accuracy and adjustable speed; each motion position can be adjusted according to actual conditions to ensure finished guard plates fall smoothly into the respective stations. Stacking efficiency: approx. 10 seconds per tray.
(10) Electrical Control Cabinet
Main electrical components include PLC, servo drives, etc., using well‑known domestic and international brands.
技术规格
- Altitude
- < 1000 m
- Ambient operating temperature
- –15°C to +40°C
交易规格
- 参考价格
- USD $100000.00 - $600000.00
- 最小起订量
- 1套
- 交货期
- 60天
- 供货能力
- 1套/周
- 装运港
- qingdao/Khorgos

山东盛源工业装备有限公司
山东盛源工业装备有限公司(简称 “盛源工业”),系中国 500 强山东融汇集团旗下子公司,始创于 1997 年,注册资本 3.6843 亿元。企业传承 “落陵精神”,秉持 “服务社会、创造价值、成就员工” 的使命,深耕矿用机械智能化领域,主营矿用支护设备、锂电池单轨吊、液压元件、工业流体控制装置等产品的研发与生产,现有 5 家下属公司。 公司为国家高新技术企业、专精特新 “小巨人”、山东瞪羚企业,坐拥 6 大生产基地,员工近 300 人。近两年营收年均增速 17.87%,2025 年营收达 4.94 亿元。公司技术实力雄厚,手握 92 项专利、百余项科创成果,多项技术达国际、国内领先水平,多项产品获省级认证;累计研发投入近 2500 万元,同时规划 29 亿元高端装备制造项目,发展潜力突出。
- 所在地
- 山东省济宁市邹城市北宿镇恒发路1号
- 主营产品
- 新型支护产品, 锂电池单轨吊, 矿用支护装备, 液压动力机械及元件, 合金铸件, 阀, 液压马达
- 员工人数
- 101-500 人
- 工厂面积
- 50,000 m² 以上
- 年销售额
- 5000 万美元以上
- 主要市场
- 东南亚 / 中东与北非